
In the pharmaceutical industry, the word 'purity' isn't just a goal—it is a legal and ethical requirement. One of the most critical processes in drug manufacturing is Solvent Recovery. Because pharmaceutical solvents are expensive and environmentally sensitive, recovering them for reuse is both a financial necessity and a sustainability mandate. At Aera Engineering Pvt Ltd, we specialize in the high-performance hardware that makes this recovery possible. Here is why the quality of your tower internals—specifically your packing and distributors—can make or break your pharmaceutical production line. 1. Ensuring Ultra-High Purity Levels Pharmaceutical solvents, such as ethanol, methanol, or acetone, must be recovered at incredibly high concentrations (often $>99.9%$). Even a few parts per million (PPM) of cross-contamination can ruin an entire batch of life-saving medicine. The Role of Internals: High-quality tower internals, like Structured Packing or precision-engineered Pall Rings, provide the massive surface area required for 'sharp' separations. The Aera Advantage: Our internals are designed to eliminate 'stagnant zones' where old solvent can hide and contaminate new batches. 2. Preventing Batch-to-Batch Contamination Pharmaceutical plants often switch between different products. This requires the distillation column to be thoroughly cleaned between runs. Surface Finish Matters: Low-quality internals often have rough surfaces or 'pockets' where chemicals can trap. Electropolished Internals: At Aera Engineering, we offer internals with superior surface finishes (often electropolished). This ensures that liquid drains completely and that CIP (Clean-In-Place) systems can reach every millimeter of the material, ensuring zero cross-contamination. 3. Handling Heat-Sensitive Compounds Many pharmaceutical solvents contain active ingredients that are thermolabile (sensitive to heat). If the solvent recovery process requires high temperatures for too long, the product may degrade. Reducing Residence Time: High-quality internals allow for a lower Pressure Drop ($Delta P$). Lower Boiling Points: By reducing the pressure drop across the column, the boiling point of the solvent is lowered. This allows the recovery to happen at a cooler temperature, protecting the integrity of heat-sensitive pharmaceutical compounds. 4. Maximizing Yield and Reducing Waste In the pharma world, every drop of solvent recovered is money saved. Low-quality tower internals often suffer from Liquid Channeling, where the solvent bypasses the gas stream entirely and exits as waste. Precision Distribution: Aera Engineering’s high-precision Liquid Distributors ensure that the solvent is spread perfectly across the packing. This maximizes the contact between the liquid and vapor, ensuring that you recover the maximum possible volume of solvent from every liter of feed. 5. Compliance and Material Certification Pharmaceutical manufacturing is governed by strict regulatory bodies like the FDA and EMA. You cannot simply use any grade of metal inside your columns. Every component Aera Engineering supplies for pharmaceutical applications comes with: Full MTC (Mill Test Certificate): Proving the exact chemical composition of the steel. Surface Roughness Reports: Verifying that the internals meet hygiene standards. Weld Integrity Checks: Ensuring no crevices exist where bacteria or impurities could grow. Engineering for Health At Aera Engineering Pvt Ltd, we understand that our tower internals are part of a larger mission to deliver safe, effective medicine to the world. By focusing on precision, cleanability, and efficiency, we help pharmaceutical companies lower their costs while maintaining the highest possible standards of purity. In pharmaceutical recovery, the smallest internal detail creates the biggest impact on the final product. Is your solvent recovery system meeting its purity targets? Contact Aera Engineering today to discuss our specialized range of internals for the pharmaceutical and fine chemical industries.


This is your website preview.
Currently it only shows your basic business info. Start adding relevant business details such as description, images and products or services to gain your customers attention by using Boost 360 android app / iOS App / web portal.
The Purity Standard: The Importance of High-Quality Tower Internals in Pharmaceutical Solvent Recove
2026-04-21T09:33:40
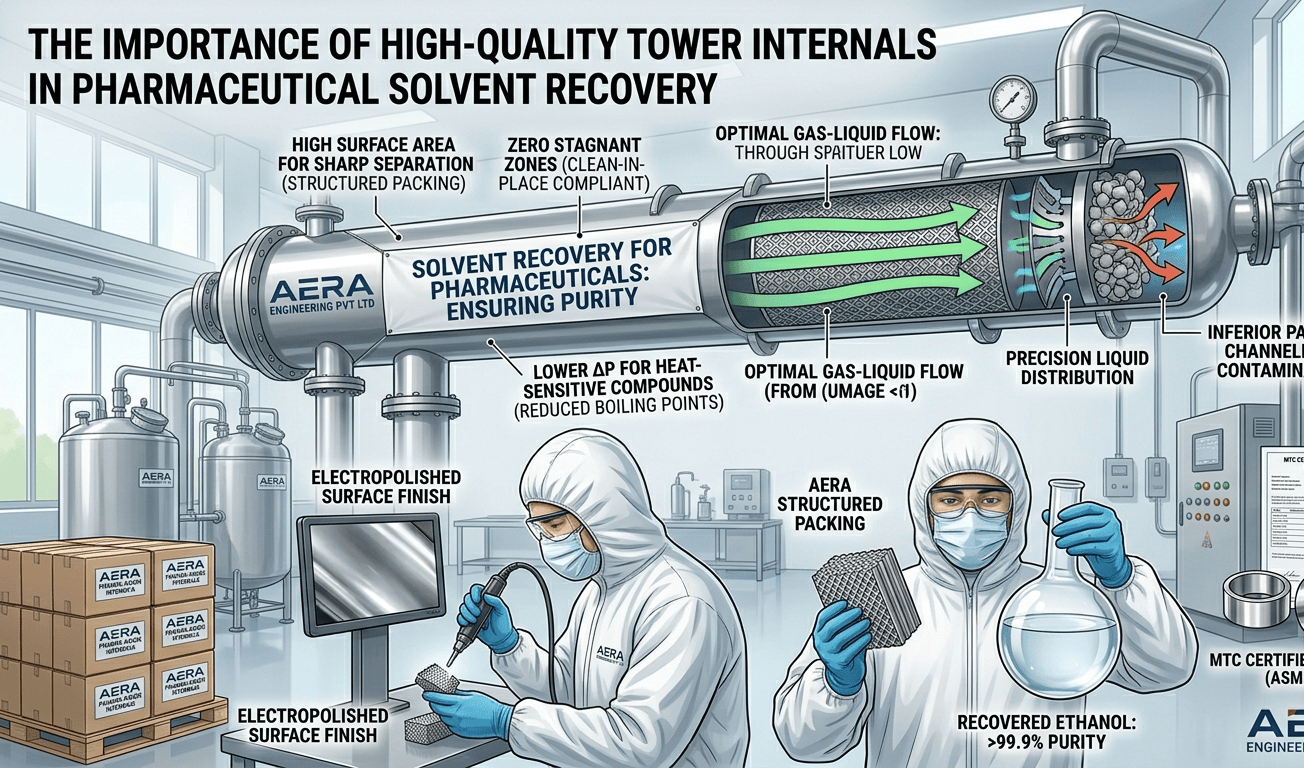
In the pharmaceutical industry, the word 'purity' isn't just a goal—it is a legal and ethical requirement. One of the most critical processes in drug manufacturing is Solvent Recovery. Because pharmaceutical solvents are expensive and environmentally sensitive, recovering them for reuse is both a financial necessity and a sustainability mandate. At Aera Engineering Pvt Ltd, we specialize in the high-performance hardware that makes this recovery possible. Here is why the quality of your tower internals—specifically your packing and distributors—can make or break your pharmaceutical production line. 1. Ensuring Ultra-High Purity Levels Pharmaceutical solvents, such as ethanol, methanol, or acetone, must be recovered at incredibly high concentrations (often $>99.9%$). Even a few parts per million (PPM) of cross-contamination can ruin an entire batch of life-saving medicine. The Role of Internals: High-quality tower internals, like Structured Packing or precision-engineered Pall Rings, provide the massive surface area required for 'sharp' separations. The Aera Advantage: Our internals are designed to eliminate 'stagnant zones' where old solvent can hide and contaminate new batches. 2. Preventing Batch-to-Batch Contamination Pharmaceutical plants often switch between different products. This requires the distillation column to be thoroughly cleaned between runs. Surface Finish Matters: Low-quality internals often have rough surfaces or 'pockets' where chemicals can trap. Electropolished Internals: At Aera Engineering, we offer internals with superior surface finishes (often electropolished). This ensures that liquid drains completely and that CIP (Clean-In-Place) systems can reach every millimeter of the material, ensuring zero cross-contamination. 3. Handling Heat-Sensitive Compounds Many pharmaceutical solvents contain active ingredients that are thermolabile (sensitive to heat). If the solvent recovery process requires high temperatures for too long, the product may degrade. Reducing Residence Time: High-quality internals allow for a lower Pressure Drop ($Delta P$). Lower Boiling Points: By reducing the pressure drop across the column, the boiling point of the solvent is lowered. This allows the recovery to happen at a cooler temperature, protecting the integrity of heat-sensitive pharmaceutical compounds. 4. Maximizing Yield and Reducing Waste In the pharma world, every drop of solvent recovered is money saved. Low-quality tower internals often suffer from Liquid Channeling, where the solvent bypasses the gas stream entirely and exits as waste. Precision Distribution: Aera Engineering’s high-precision Liquid Distributors ensure that the solvent is spread perfectly across the packing. This maximizes the contact between the liquid and vapor, ensuring that you recover the maximum possible volume of solvent from every liter of feed. 5. Compliance and Material Certification Pharmaceutical manufacturing is governed by strict regulatory bodies like the FDA and EMA. You cannot simply use any grade of metal inside your columns. Every component Aera Engineering supplies for pharmaceutical applications comes with: Full MTC (Mill Test Certificate): Proving the exact chemical composition of the steel. Surface Roughness Reports: Verifying that the internals meet hygiene standards. Weld Integrity Checks: Ensuring no crevices exist where bacteria or impurities could grow. Engineering for Health At Aera Engineering Pvt Ltd, we understand that our tower internals are part of a larger mission to deliver safe, effective medicine to the world. By focusing on precision, cleanability, and efficiency, we help pharmaceutical companies lower their costs while maintaining the highest possible standards of purity. In pharmaceutical recovery, the smallest internal detail creates the biggest impact on the final product. Is your solvent recovery system meeting its purity targets? Contact Aera Engineering today to discuss our specialized range of internals for the pharmaceutical and fine chemical industries.
2026-04-21T09:33:40


Keywords
- Top rated IMTP saddles in India
- Aera Engineering tower packing solutions
- Low pressure drop IMTP saddle specifications
- Corrosion-resistant random packing for chemical plants
- Tower packing for petrochemical distillation India
- Equivalent CMR rings for VOC removal
- High-efficiency IMTP packing for solvent recovery
- SS 316L Pall Rings for acid scrubbing
- Custom CMR ring design services
- Plastic Pall Ring 50mm price India
- Industrial tower internals price list
- Metal CMR rings for distillation columns India
- Bulk IMTP saddle tower packing for sale
- Stainless Steel Pall Ring price per piece
- Mass transfer equipment manufacturers in Mumbai
- Random packing suppliers in Vadodara
- Random packing suppliers in India
- Random packing suppliers in Pune
- CMR rings price in India
- Tower packing manufacturers near me
- IMTP saddle suppliers in Gujarat
- Pall rings manufacturer in Vadodara
- pharmaceutical solvent recovery high purity
- tower internals structured packing distributor
- electropolished internals Clean-In-Place
- low pressure drop solvent recovery
- FDA EMA compliant tower internals
Submit Your Enquiry